PRODUCT OVERVIEW
Designed around the production task.
A high-efficiency single-screw extruder for pipe applications requiring stable output, controlled melt quality and energy awareness.
EQUIPMENT REFERENCE
Confirmed equipment, followed by the process context.
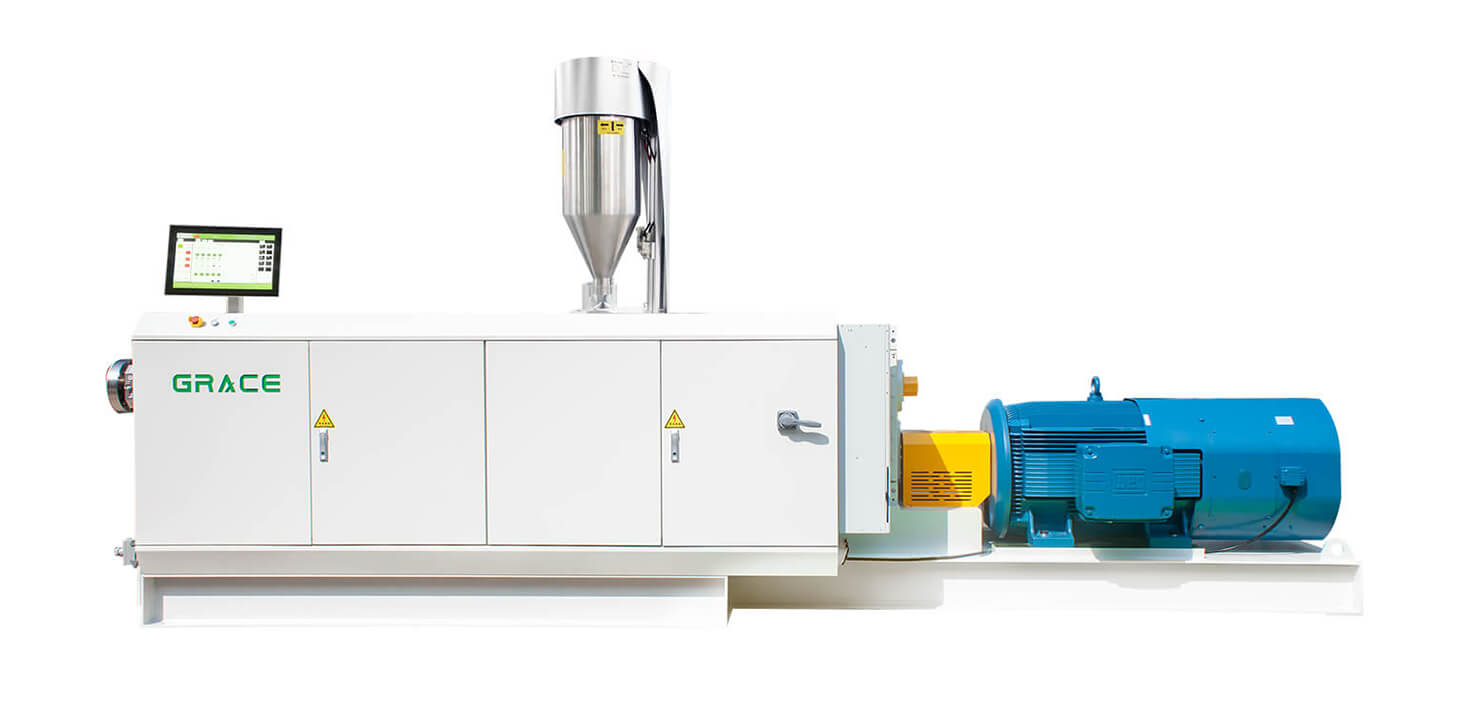
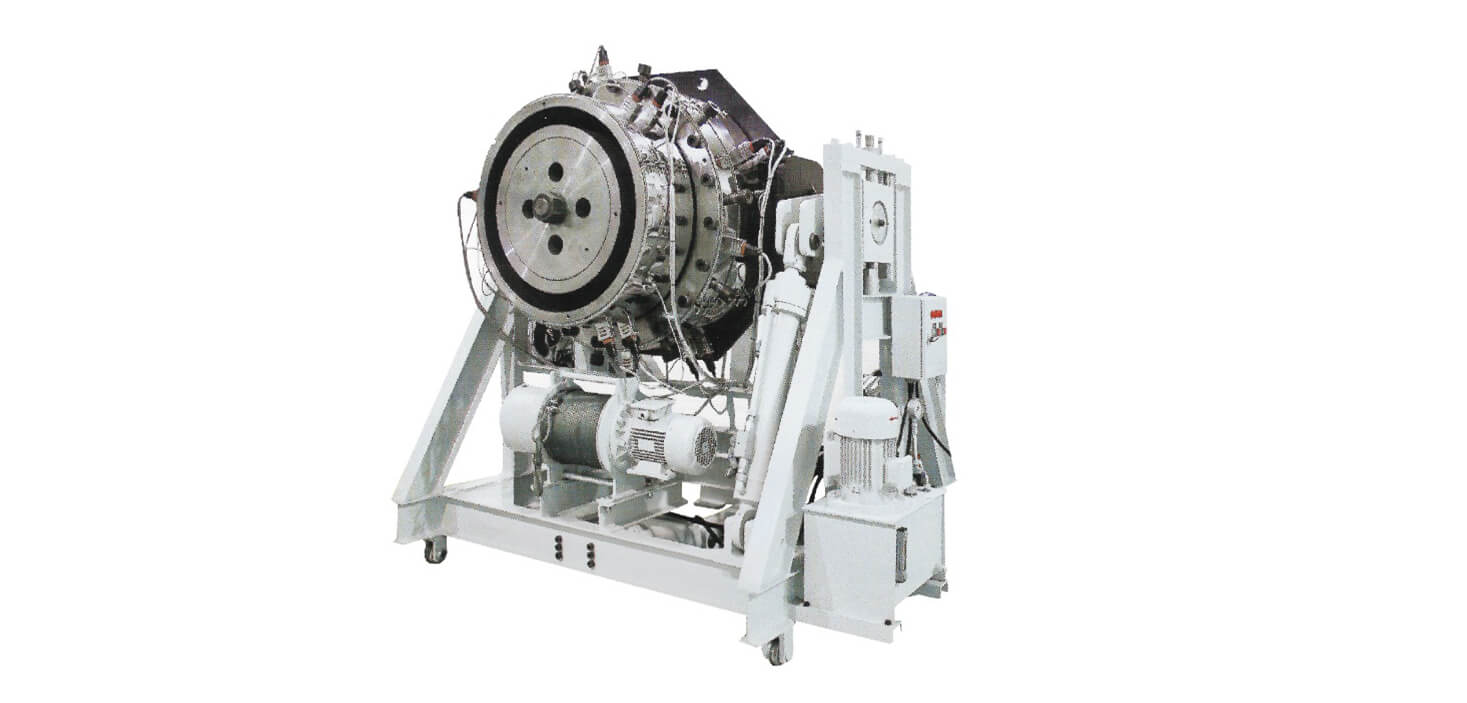
40 L/D single-screw extruder
The 40 L/D SG single-screw extruder is engineered for large-diameter and thick-wall pipe applications. Its screw design and process control support melt homogeneity, pressure stability, cooling efficiency and controlled wall thickness during extrusion.
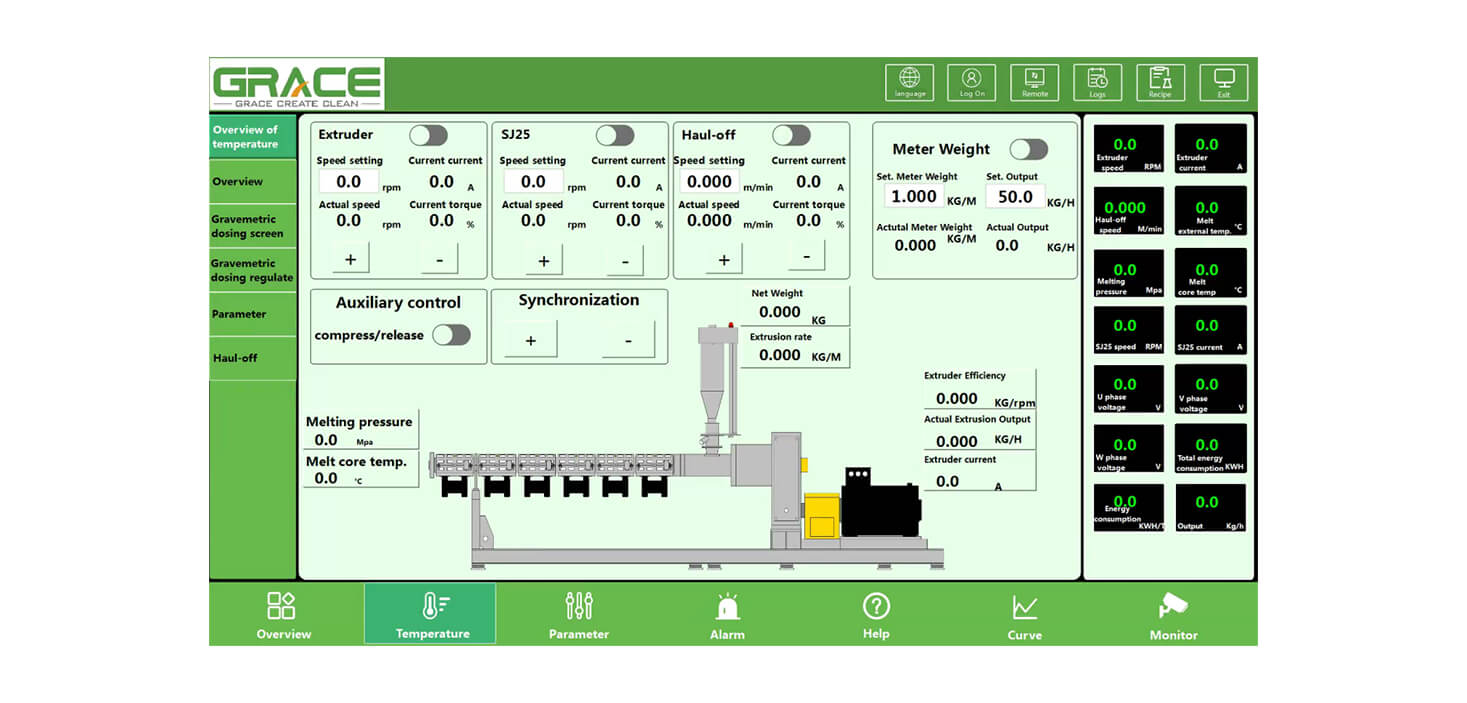
Process control
The control arrangement brings key operating values together to support practical start-up, repeatable operation and day-to-day process monitoring. Final controls and interfaces are defined for the selected line configuration.
Project-specific verification
Extruder selection and final line performance are verified against the resin grade, die, pipe specification, cooling capacity and downstream process. Published reference values are not an unconditional contractual guarantee.
CONFIGURATION ENGINEERING
Configuring the HDPE / PP extrusion platform as part of the full line
The 40 L/D single-screw extruder is defined with the resin, pipe structure, die head, cooling route and downstream duty. It provides the melt-preparation platform; final line performance depends on every connected production stage.
Resin & pipe structure
PE or PP grade, pipe application, wall schedule and single- or multi-layer structure guide the screw, drive and control concept. These material inputs are reviewed before the platform is fixed.
Melt preparation & die interface
Screw geometry, thermal control and the die-head interface are aligned for the selected resin and pipe range. Co-extrusion and stripe arrangements are reviewed with the complete product definition.
Cooling & downstream balance
The extruder is balanced with the available cooling length, water conditions, haul-off capacity and cutting cycle. A machine value alone is never used to define final stable line output.
Line integration
Material handling, process control, measurement and auxiliary interfaces are specified as part of the complete line. The final control and service scope follows the selected project configuration.
FOR A TECHNICAL PROPOSAL
Information that lets us define the right line.
- Resin grade and intended application
- Complete OD × SDR or wall-thickness schedule
- Layer structure, stripe and co-extrusion requirements
- Target operating rate by key pipe size
- Cooling-water and factory-layout conditions
- Control, measurement and service requirements
Published model information is a planning reference, not an unconditional promise. Final output, melt condition, energy use and product performance are verified for the agreed resin, tooling and complete production line.
TECHNICAL DATA
40 L/D single-screw extruder model range
| Model | Application | Screw diameter | L/D | Main motor | Reference output — stable / nominal / upper |
|---|---|---|---|---|---|
| GMSE60/40-A200 | PE / HDPE pipe | 60 mm | 40 | 200 kW | 700 / 750 / 800 kg/h |
| GMSE75/40-A315 | PE / HDPE pipe | 75 mm | 40 | 315 kW | 1,000 / 1,100 / 1,200 kg/h |
| GMSE90/40-A450 | PE / HDPE pipe | 90 mm | 40 | 450 kW | 1,600 / 1,700 / 1,800 kg/h |
GMSE60/40-A200
- Application
- PE / HDPE pipe
- Screw diameter
- 60 mm
- L/D
- 40
- Main motor
- 200 kW
- Reference output — stable / nominal / upper
- 700 / 750 / 800 kg/h
GMSE75/40-A315
- Application
- PE / HDPE pipe
- Screw diameter
- 75 mm
- L/D
- 40
- Main motor
- 315 kW
- Reference output — stable / nominal / upper
- 1,000 / 1,100 / 1,200 kg/h
GMSE90/40-A450
- Application
- PE / HDPE pipe
- Screw diameter
- 90 mm
- L/D
- 40
- Main motor
- 450 kW
- Reference output — stable / nominal / upper
- 1,600 / 1,700 / 1,800 kg/h
Reference outputs are preliminary extruder-selection values, not guaranteed complete-line output. Final performance depends on resin grade, melt-flow characteristics, die and pipe specification, cooling capacity, line speed and downstream limits, and must be confirmed through project-level technical review and FAT criteria.