SEE IT IN OPERATION
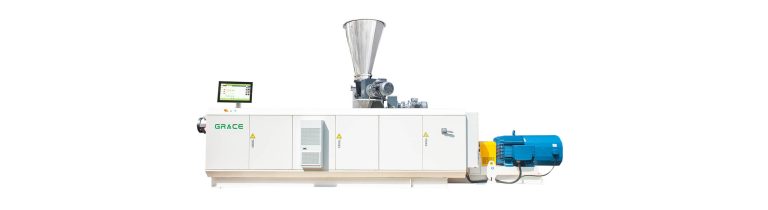
Parallel Twin-Screw Extruder (36 L/D)
Start with the equipment in operation, then explore the principal functions and the relevant technical configuration.
PRODUCT OVERVIEW
Designed around the production task.
A parallel twin-screw platform for controlled PVC processing, supporting stable melt quality and flexible line configuration.
EQUIPMENT REFERENCE
Confirmed equipment, followed by the process context.
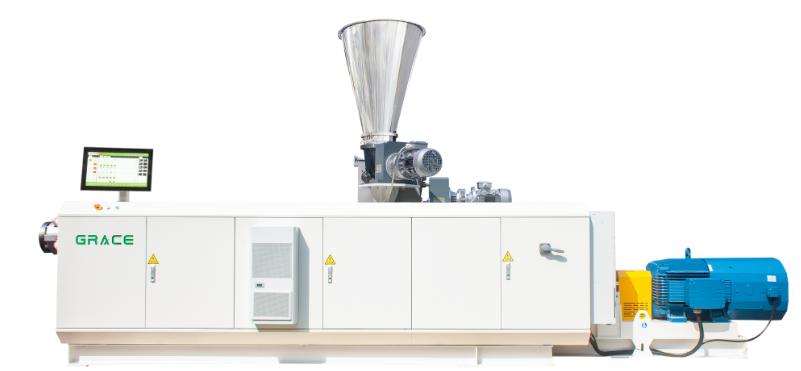
Parallel Twin Screw Extruders for Grace Equipment
As the demand for efficient and high-quality plastic pipe extrusion escalates, so does the need for advanced equipment that ensures consistent performance and precision control. At Grace, we recognize the challenges faced by plastic pipe manufacturers and our Twin Screw Extruders stand as the optimal solution for rapid, reliable production. Key Features The core advantage of parallel twin screw extruders lies in their ability to deliver high-output, precision-contro
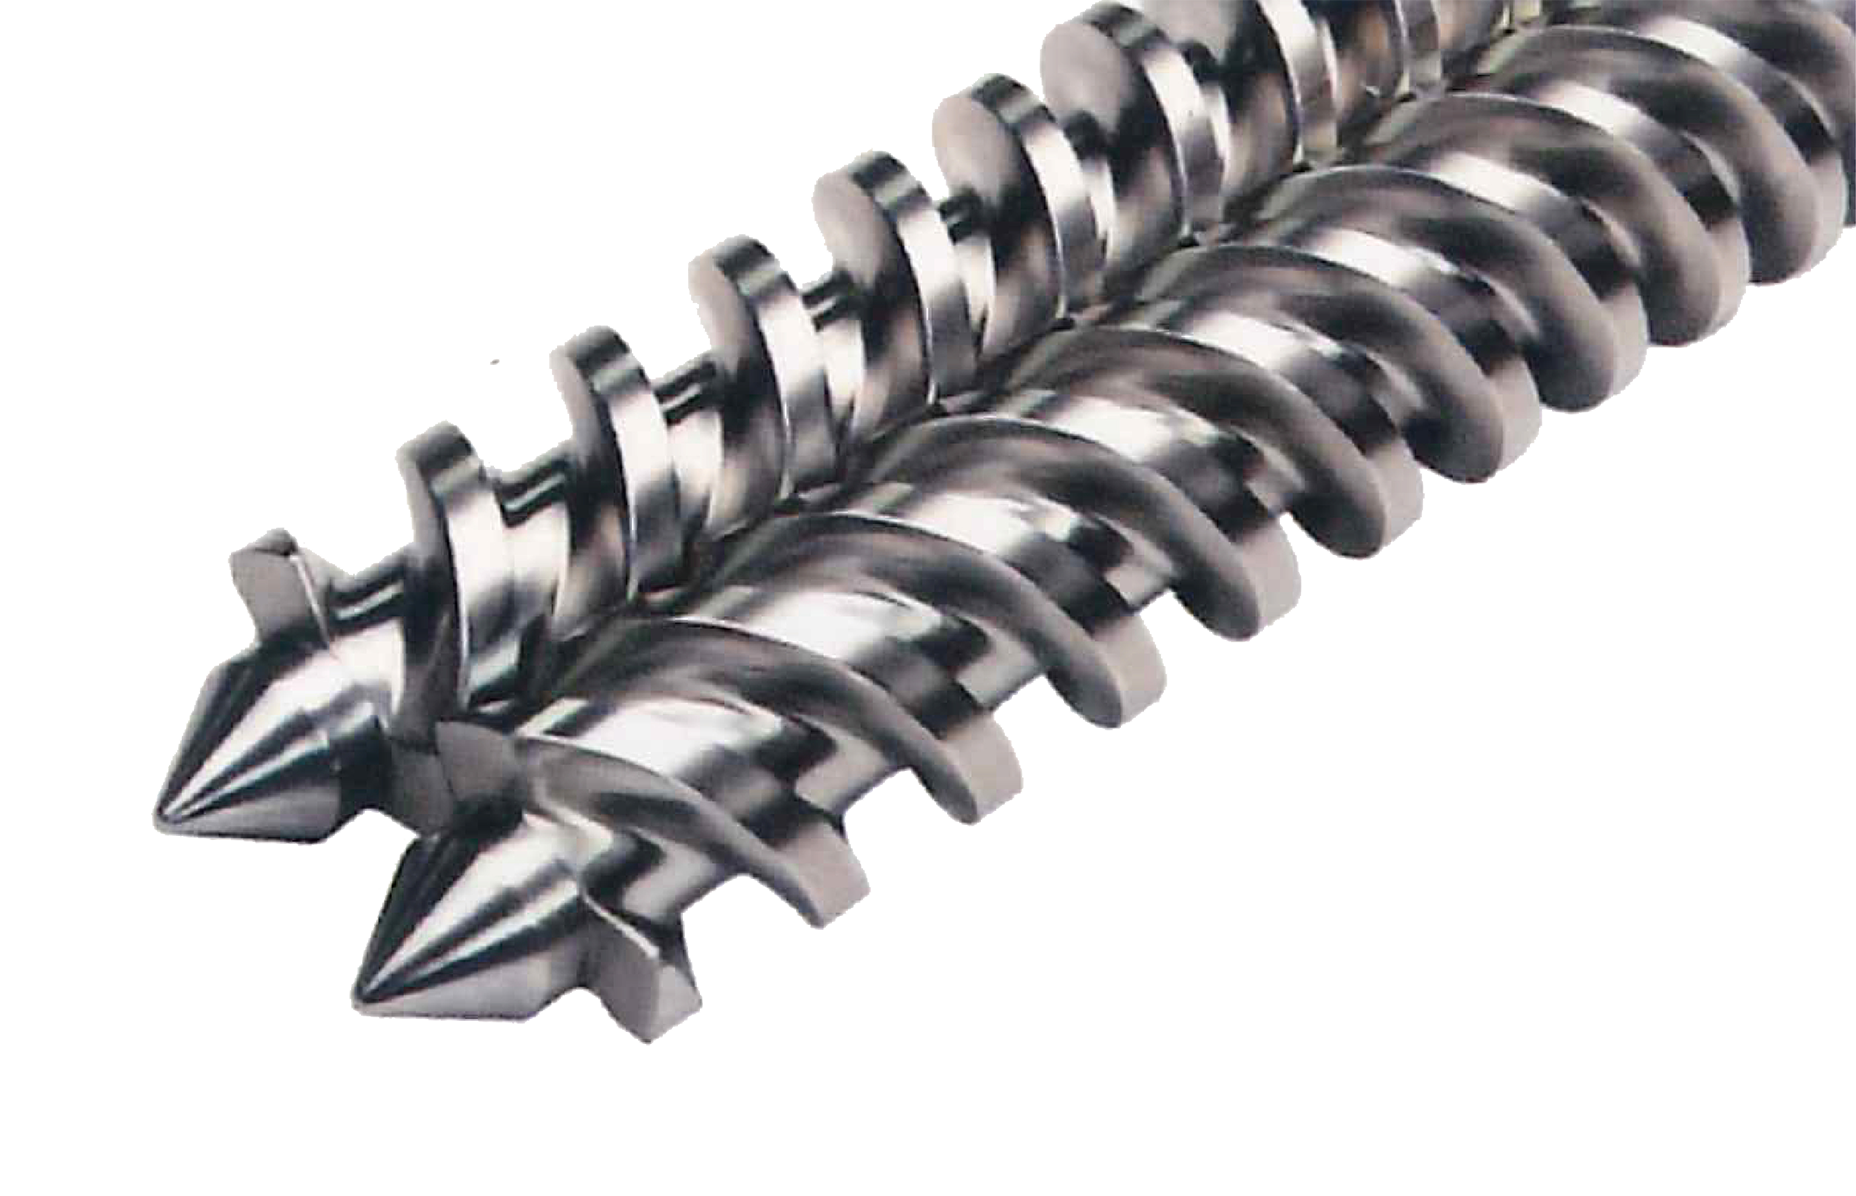
Optimized Screw Geometry: Your Gateway to Extrusion Excellence
Grace’s Twin Screw Extruders feature an enhanced screw design with extended effective length, delivering: Homogeneous Melt Quality: Ensures uniform material properties and surface finish. Expanded Processing Flexibility: Accommodates diverse polymers and additives with precision. 30% Lower Reject Rates: Minimizes waste and maximizes yield, directly improving your bottom line. Experience the difference of smarter screw engineering—where innovation meets efficiency.
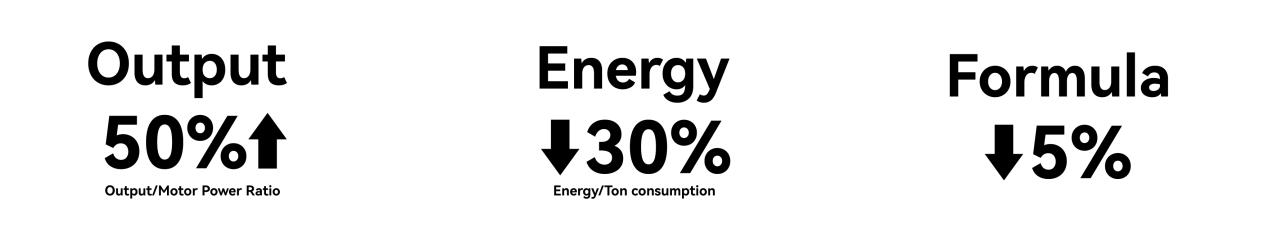
Intelligent Operational Control Panel: Engineered for Productivity & Profitability
Our smart control interface redefines operational efficiency by merging intuitive functionality with data-driven insights, delivering tangible value at every production stage:
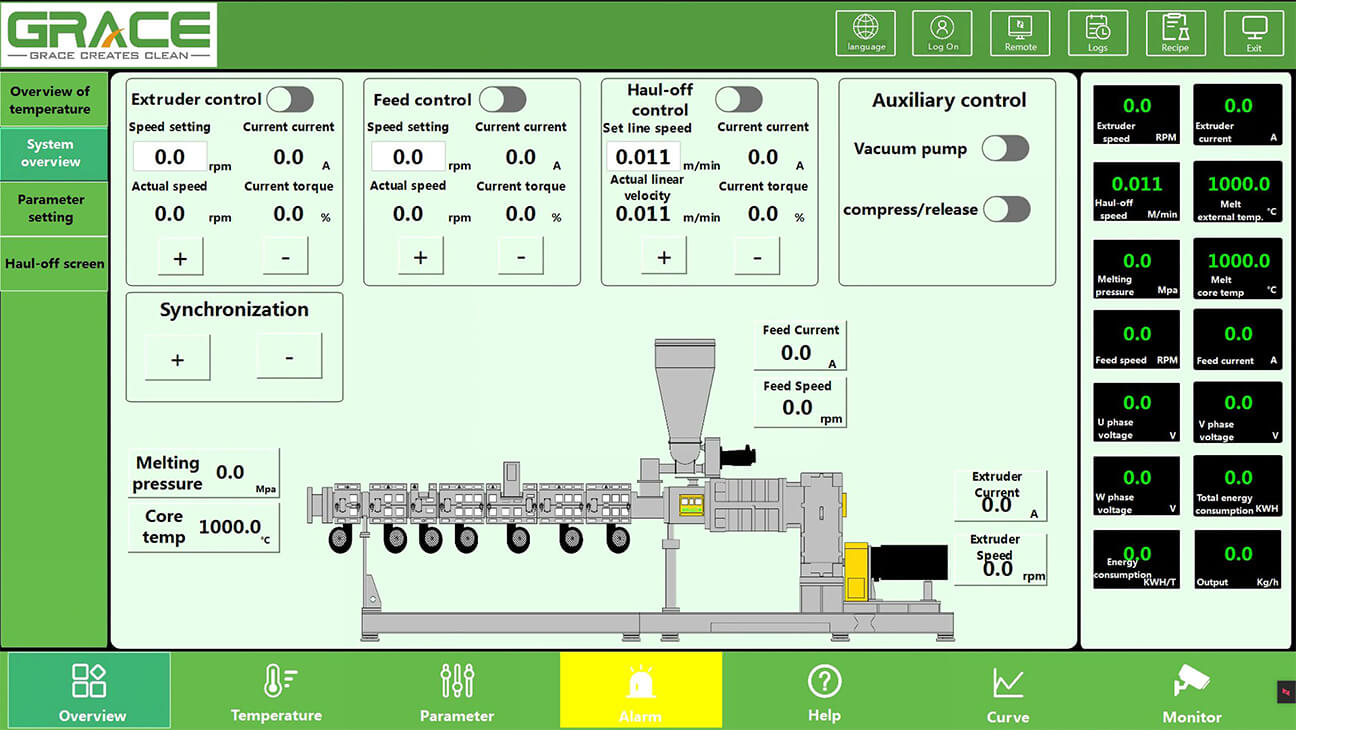
Triple Threat of Operational Excellence
Real-Time Data Hub Displays critical metrics (speed, temperature, pressure) in intuitive dashboards, enabling operators to detect anomalies within seconds. Proactive monitoring reduces quality defects by 30% and minimizes rework costs. Remote IoT Diagnostics Connects to your plant’s network for remote monitoring. Instant SMS alerts for equipment faults cut downtime by 50%, while cloud-based diagnostics allow our engineers to resolve 60% of issues without onsite visi
Product description:
Extruder Mode Max.Output(kg/h) Pipe Range(mm) Power(kw) GMPT 75/36 400-500 50-160,110-250 45 GMPT 90/36 650-800 160-315,250-400 75 GMPT 114/36 900-1200 315-630,400-800 110 GMPT 135/36 1200-1600 800-1200 160
CONFIGURATION ENGINEERING
Defining the PVC extrusion platform from the formulation and line duty
The parallel twin-screw extruder is the controlled melt-preparation stage of a PVC pipe line. Its configuration is considered together with the PVC formulation, finished-pipe schedule, die, cooling capacity and downstream operating duty rather than as an isolated throughput number.
PVC formulation first
Resin grade, stabiliser system, filler level, additives and the intended pipe application establish the processing conditions. These inputs are reviewed before screw, temperature and control settings are defined.
Extruder platform & process window
The 36 L/D parallel twin-screw platform is selected around the required plasticisation route, operating rate and the pipe schedule. The final drive, screw and barrel arrangement remain tied to the approved project configuration.
Die & downstream interface
Melt preparation has to match the die, calibration, cooling and haul-off sections. The line is balanced around the actual pipe wall, number of outlets and downstream conditions rather than a headline machine output.
Control & operating continuity
The control architecture brings key operating conditions together for recipe-based operation and practical changeovers. Interfaces for line control, material preparation and auxiliary equipment are defined for the selected project.
FOR A TECHNICAL PROPOSAL
Information that lets us define the right line.
- PVC formulation and intended pipe application
- Complete pipe schedule and number of outlets
- Target operating rate by key specification
- Die, calibration and downstream arrangement
- Electrical supply, control interface and factory conditions
- Automation, traceability and service requirements
Reference platform information is not a standalone production guarantee. Final stable output, energy use, process settings and finished-pipe quality are verified with the complete project line and its agreed acceptance criteria.
TECHNICAL DATA
36 L/D parallel twin-screw extruder model range
| Model | Application | Screw diameter | L/D | Main motor | Reference output — stable / nominal / upper |
|---|---|---|---|---|---|
| GMPT75/36-A45 | PVC pipe | 75 mm | 36 | 45 kW | 400 / 450 / 500 kg/h |
| GMPT90/36-A75 | PVC pipe | 90 mm | 36 | 75 kW | 640 / 720 / 800 kg/h |
| GMPT114/36-A110 | PVC pipe | 114 mm | 36 | 110 kW | 960 / 1,080 / 1,200 kg/h |
| GMPT135/36-A200 | PVC pipe | 135 mm | 36 | 200 kW | 1,280 / 1,440 / 1,600 kg/h |
GMPT75/36-A45
- Application
- PVC pipe
- Screw diameter
- 75 mm
- L/D
- 36
- Main motor
- 45 kW
- Reference output — stable / nominal / upper
- 400 / 450 / 500 kg/h
GMPT90/36-A75
- Application
- PVC pipe
- Screw diameter
- 90 mm
- L/D
- 36
- Main motor
- 75 kW
- Reference output — stable / nominal / upper
- 640 / 720 / 800 kg/h
GMPT114/36-A110
- Application
- PVC pipe
- Screw diameter
- 114 mm
- L/D
- 36
- Main motor
- 110 kW
- Reference output — stable / nominal / upper
- 960 / 1,080 / 1,200 kg/h
GMPT135/36-A200
- Application
- PVC pipe
- Screw diameter
- 135 mm
- L/D
- 36
- Main motor
- 200 kW
- Reference output — stable / nominal / upper
- 1,280 / 1,440 / 1,600 kg/h
Reference outputs require formulation review and are not unconditional guarantees. Resin K-value, stabilizer system, CaCO₃ loading, recycled-content ratio, pipe standard, die throughput and downstream cooling must be confirmed. The current model designation is GMPT135/36; historical 135/28 references are not used as the current standard.