PRODUCT OVERVIEW
Designed around the production task.
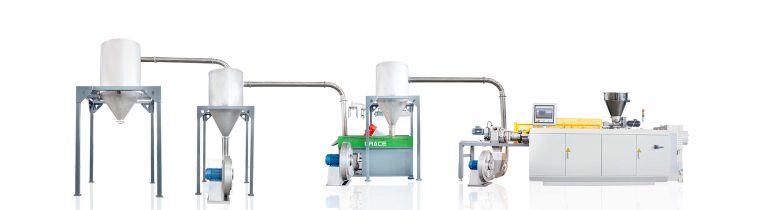
Twin-screw pelletizing for PVC compounds, configured around the material, formulation and required pellet application.
MATERIAL & PROCESS CONTEXT
Material, process and output context.
PVC compound input
The pelletizing configuration is defined around the PVC compound, formulation, feed condition and intended pellet application. These project inputs must be confirmed before equipment selection.
Twin-screw processing
The twin-screw processing stage prepares the compound for pellet formation. Screw arrangement, temperature control and downstream configuration are reviewed for the specific compound and operating requirement.
Pelletizing and cooling
Pelletizing and cooling arrangements are selected around the required pellet form and material behaviour. Final output and quality criteria are agreed through technical review and validation.
CONFIGURATION ENGINEERING
Engineering pvc pelletizing module around the actual material
A recycling system is defined from the actual feedstock and required downstream use, not from a headline model or capacity. Material condition, contamination, safety boundary and each process interface are reviewed together before a project configuration is released.
Material definition
Confirm polymer family, material form, incoming size, contamination profile, moisture, labels, metals, non-target fractions and any restricted or hazardous contents before selecting the route.
Process-route integration
The selected process interface is feeding, twin-screw processing, pelletizing and cooling. Each module is balanced with its upstream preparation, downstream handling and the declared target material requirement.
Utilities, residue and safety
Water management, residue handling, ventilation, access, guarding and site constraints are defined with the actual material and local operating conditions; they are not assumed from a generic reference line.
Project confirmation
The final equipment list, operating window, controls and acceptance criteria are confirmed through project engineering, controlled technical review and the agreed validation plan.
FOR A TECHNICAL PROPOSAL
Information that lets us define the right line.
- Formulation, feed condition, pellet requirement, utilities and quality criteria
- Clear material photos or representative samples, including packaging and contamination condition
- Required target material, downstream use and any purity, moisture or handling expectations
- Factory layout, utilities, water-treatment boundary, safety rules and local regulatory requirements
- Required controls, service access, documentation language and project delivery expectations
This v2 Beta page presents the R&D-signed technical reference for the stated material and process scope. It is not a price, delivery, quality, certification or contractual performance commitment; the final project configuration and acceptance conditions remain subject to controlled engineering review.
TECHNICAL DATA
Representative PVC pelletizing configurations
| Model | Primary role | Applicable feedstock / condition | Candidate route capacity range | Key standard configuration | Selection boundary |
|---|---|---|---|---|---|
| 80/156 conical twin-screw | PVC plasticising and extrusion | PVC compound; formulation, feed form and moisture to be confirmed | 350–400 kg/h | Ceramic heating · vacuum system · feeding system · paired with 250 die-face hot cutting | Reference configuration only; final formula, pellet requirement, utilities and validation remain project-specific. |
| 92/188 conical twin-screw | PVC plasticising and extrusion | PVC compound; formulation, feed form and moisture to be confirmed | 500–700 kg/h | Ceramic heating · vacuum system · feeding system · paired with 330 die-face hot cutting | Reference configuration only; final formula, pellet requirement, utilities and validation remain project-specific. |
| 135/33 counter-rotating parallel twin-screw | PVC plasticising and extrusion | PVC compound; formulation, feed form and moisture to be confirmed | 1,000–1,500 kg/h | Ceramic heating · vacuum system · feeding system · paired with 330 die-face hot cutting | Reference configuration only; final formula, pellet requirement, utilities and validation remain project-specific. |
80/156 conical twin-screw
- Primary role
- PVC plasticising and extrusion
- Applicable feedstock / condition
- PVC compound; formulation, feed form and moisture to be confirmed
- Candidate route capacity range
- 350–400 kg/h
- Key standard configuration
- Ceramic heating · vacuum system · feeding system · paired with 250 die-face hot cutting
- Selection boundary
- Reference configuration only; final formula, pellet requirement, utilities and validation remain project-specific.
92/188 conical twin-screw
- Primary role
- PVC plasticising and extrusion
- Applicable feedstock / condition
- PVC compound; formulation, feed form and moisture to be confirmed
- Candidate route capacity range
- 500–700 kg/h
- Key standard configuration
- Ceramic heating · vacuum system · feeding system · paired with 330 die-face hot cutting
- Selection boundary
- Reference configuration only; final formula, pellet requirement, utilities and validation remain project-specific.
135/33 counter-rotating parallel twin-screw
- Primary role
- PVC plasticising and extrusion
- Applicable feedstock / condition
- PVC compound; formulation, feed form and moisture to be confirmed
- Candidate route capacity range
- 1,000–1,500 kg/h
- Key standard configuration
- Ceramic heating · vacuum system · feeding system · paired with 330 die-face hot cutting
- Selection boundary
- Reference configuration only; final formula, pellet requirement, utilities and validation remain project-specific.
The capacities are controlled source references for the listed PVC configurations, not unconditional customer commitments. Formula, feed moisture, pellet specification, cooling, filtration, quality requirements and validation define the final project configuration.