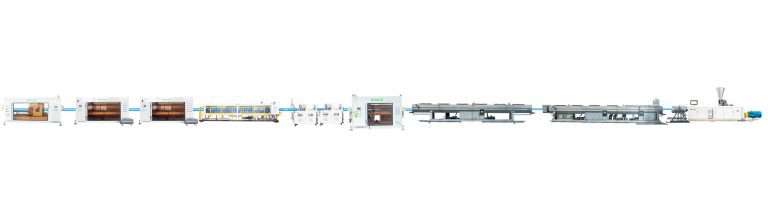
SEE IT IN OPERATION
PVC-O Pipe Extrusion Line
Start with the equipment in operation, then explore the principal functions and the relevant technical configuration.
PRODUCT OVERVIEW
Designed around the production task.
PVC-O pipe extrusion technology combining controlled processing with dependable dimensional performance for modern pipe production.
EQUIPMENT REFERENCE
Confirmed equipment, followed by the process context.
 Explore this equipment →
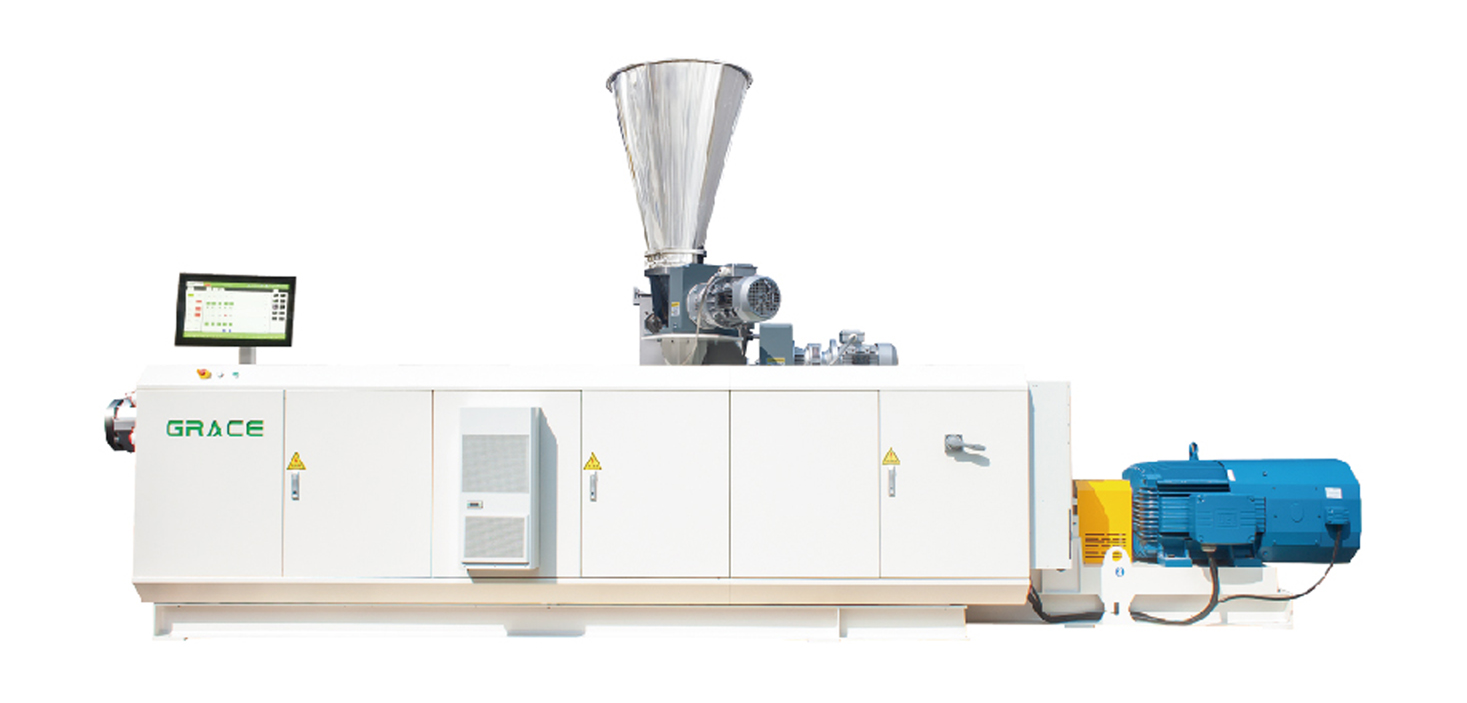
Parallel twin-screw extruder
The 36 L/D parallel twin-screw extruder provides the controlled PVC melt preparation required for a stable preform pipe before orientation.
View equipment page →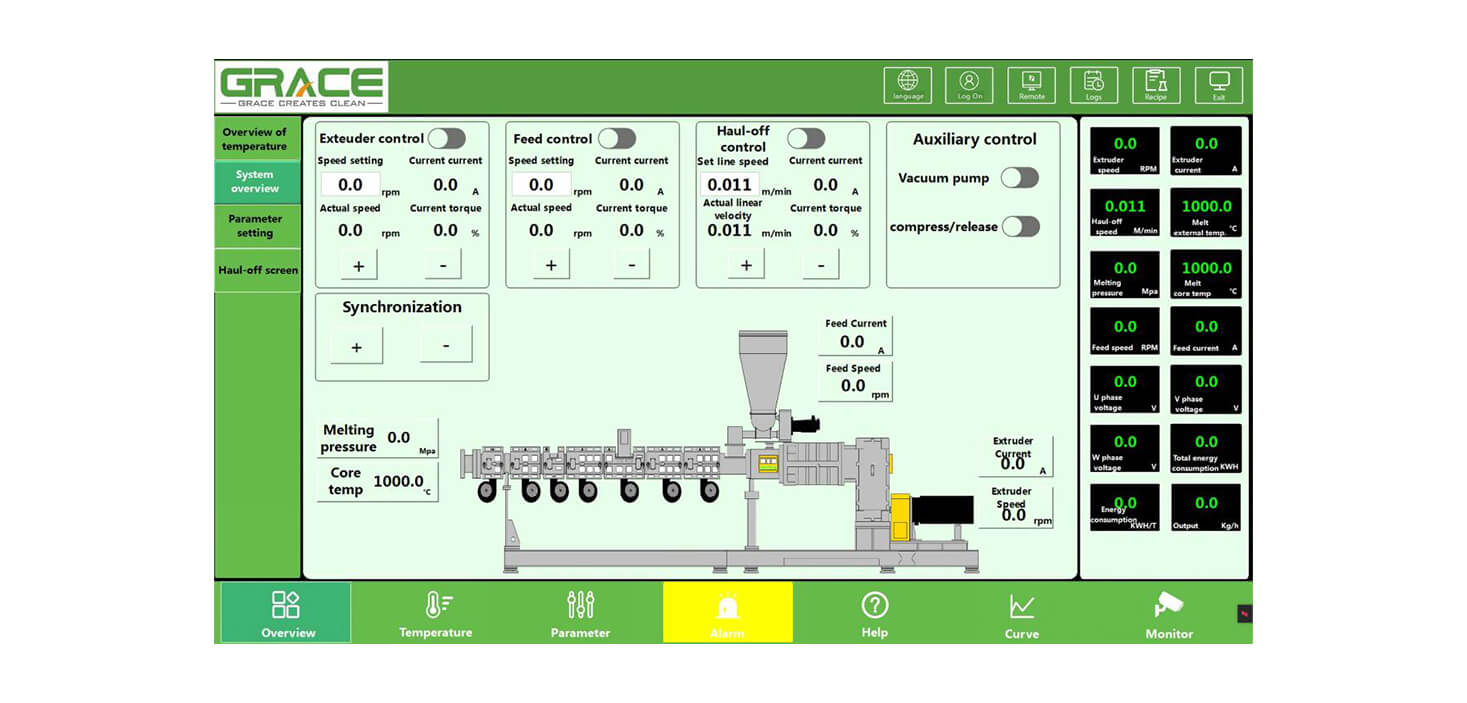
PLC control system
Centralised line control coordinates the principal process parameters and provides operators with a clear view of the production process.
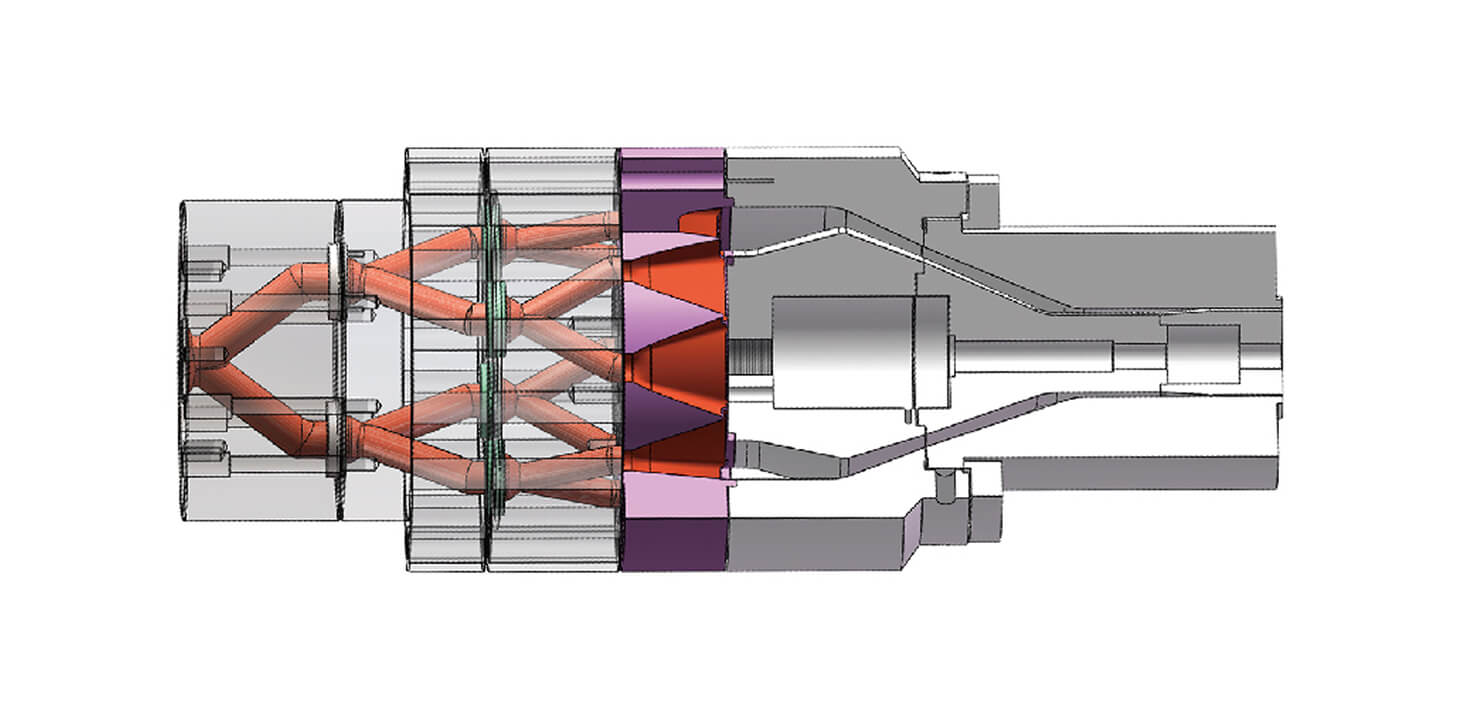
Die head
The die-head design supports controlled melt distribution and a stable preform pipe profile before the in-line orientation process begins.
 Explore this equipment →
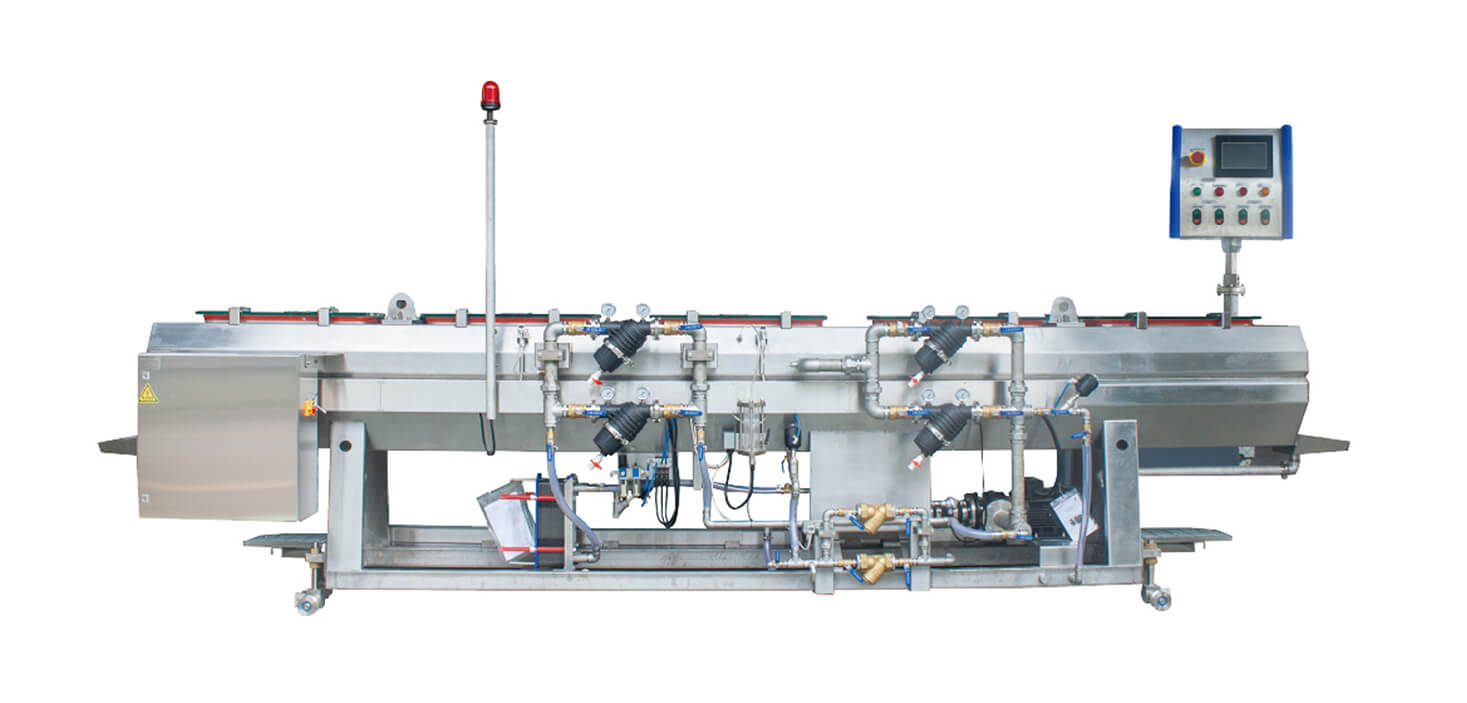
Vacuum tank
Vacuum and cooling are configured for stable preform geometry, controlled water management and practical maintenance access.
View equipment page →Preform pipe haul-off
Independent servo drives and high-friction rubber blocks help maintain controlled preform traction before the pipe enters the orientation stations.
View equipment page →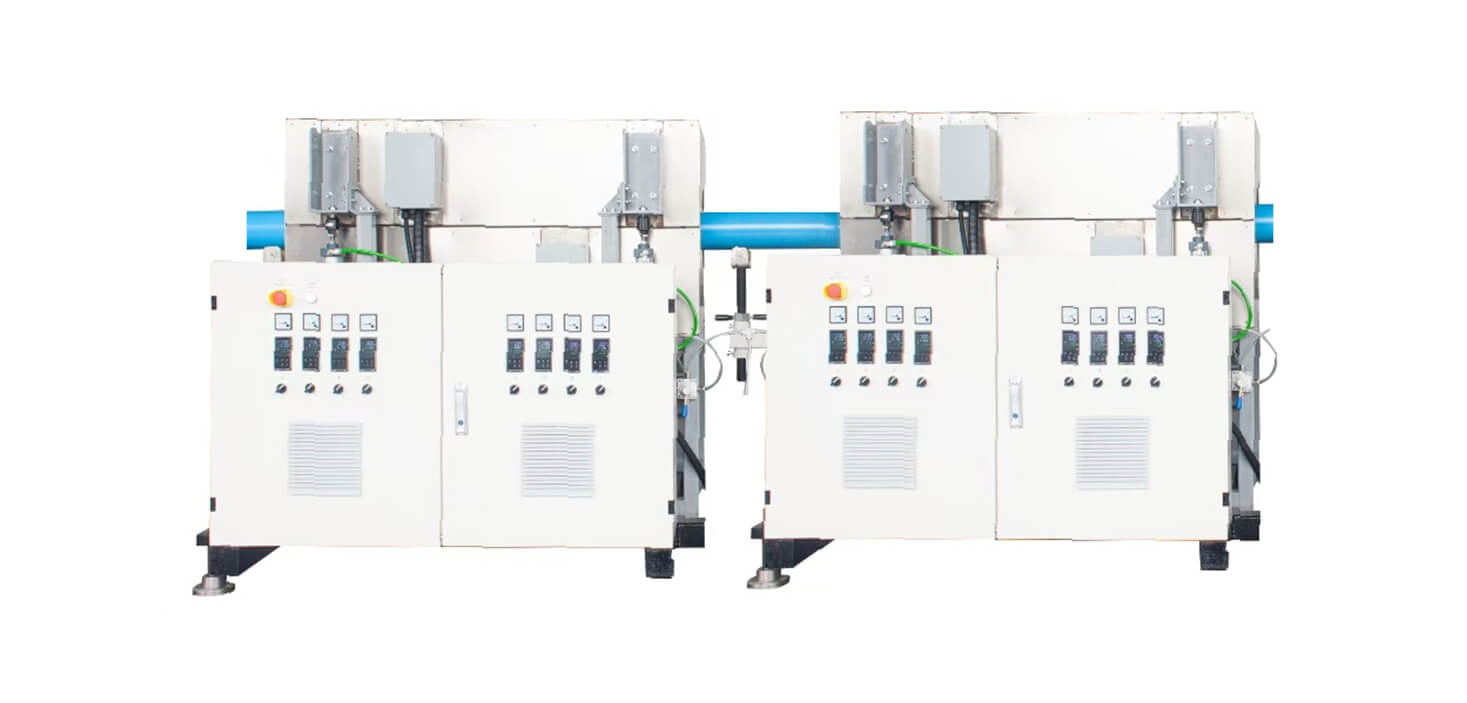
Infrared heating
Independent heating zones and automatic temperature adjustment bring the preform pipe to the required orientation temperature with responsive control.
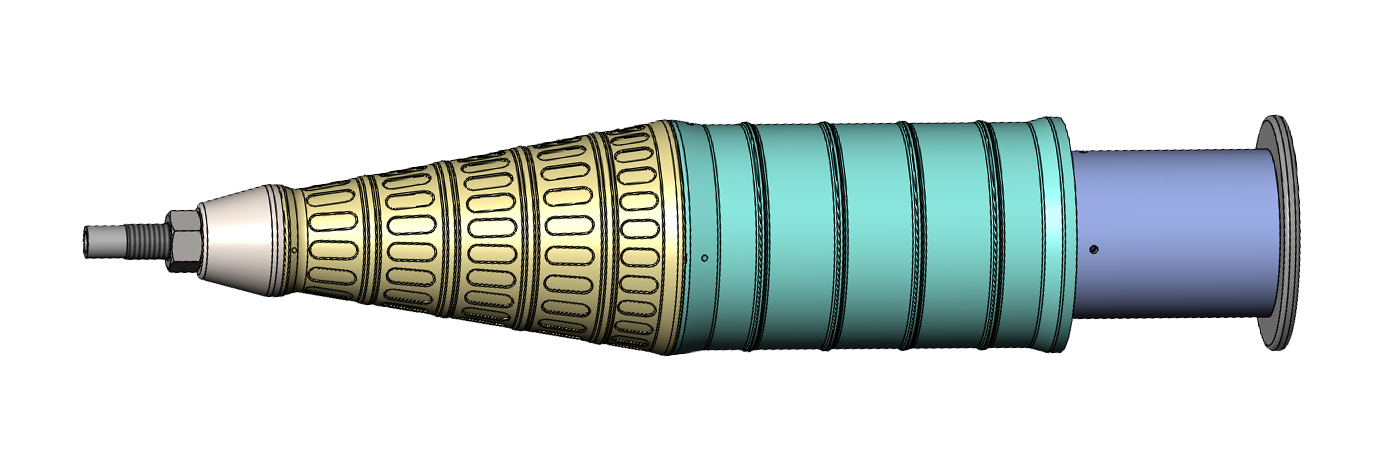
Biaxial orientation station
The in-line orientation process combines radial expansion and axial stretching to form the ordered molecular structure required for PVC-O pipe production.
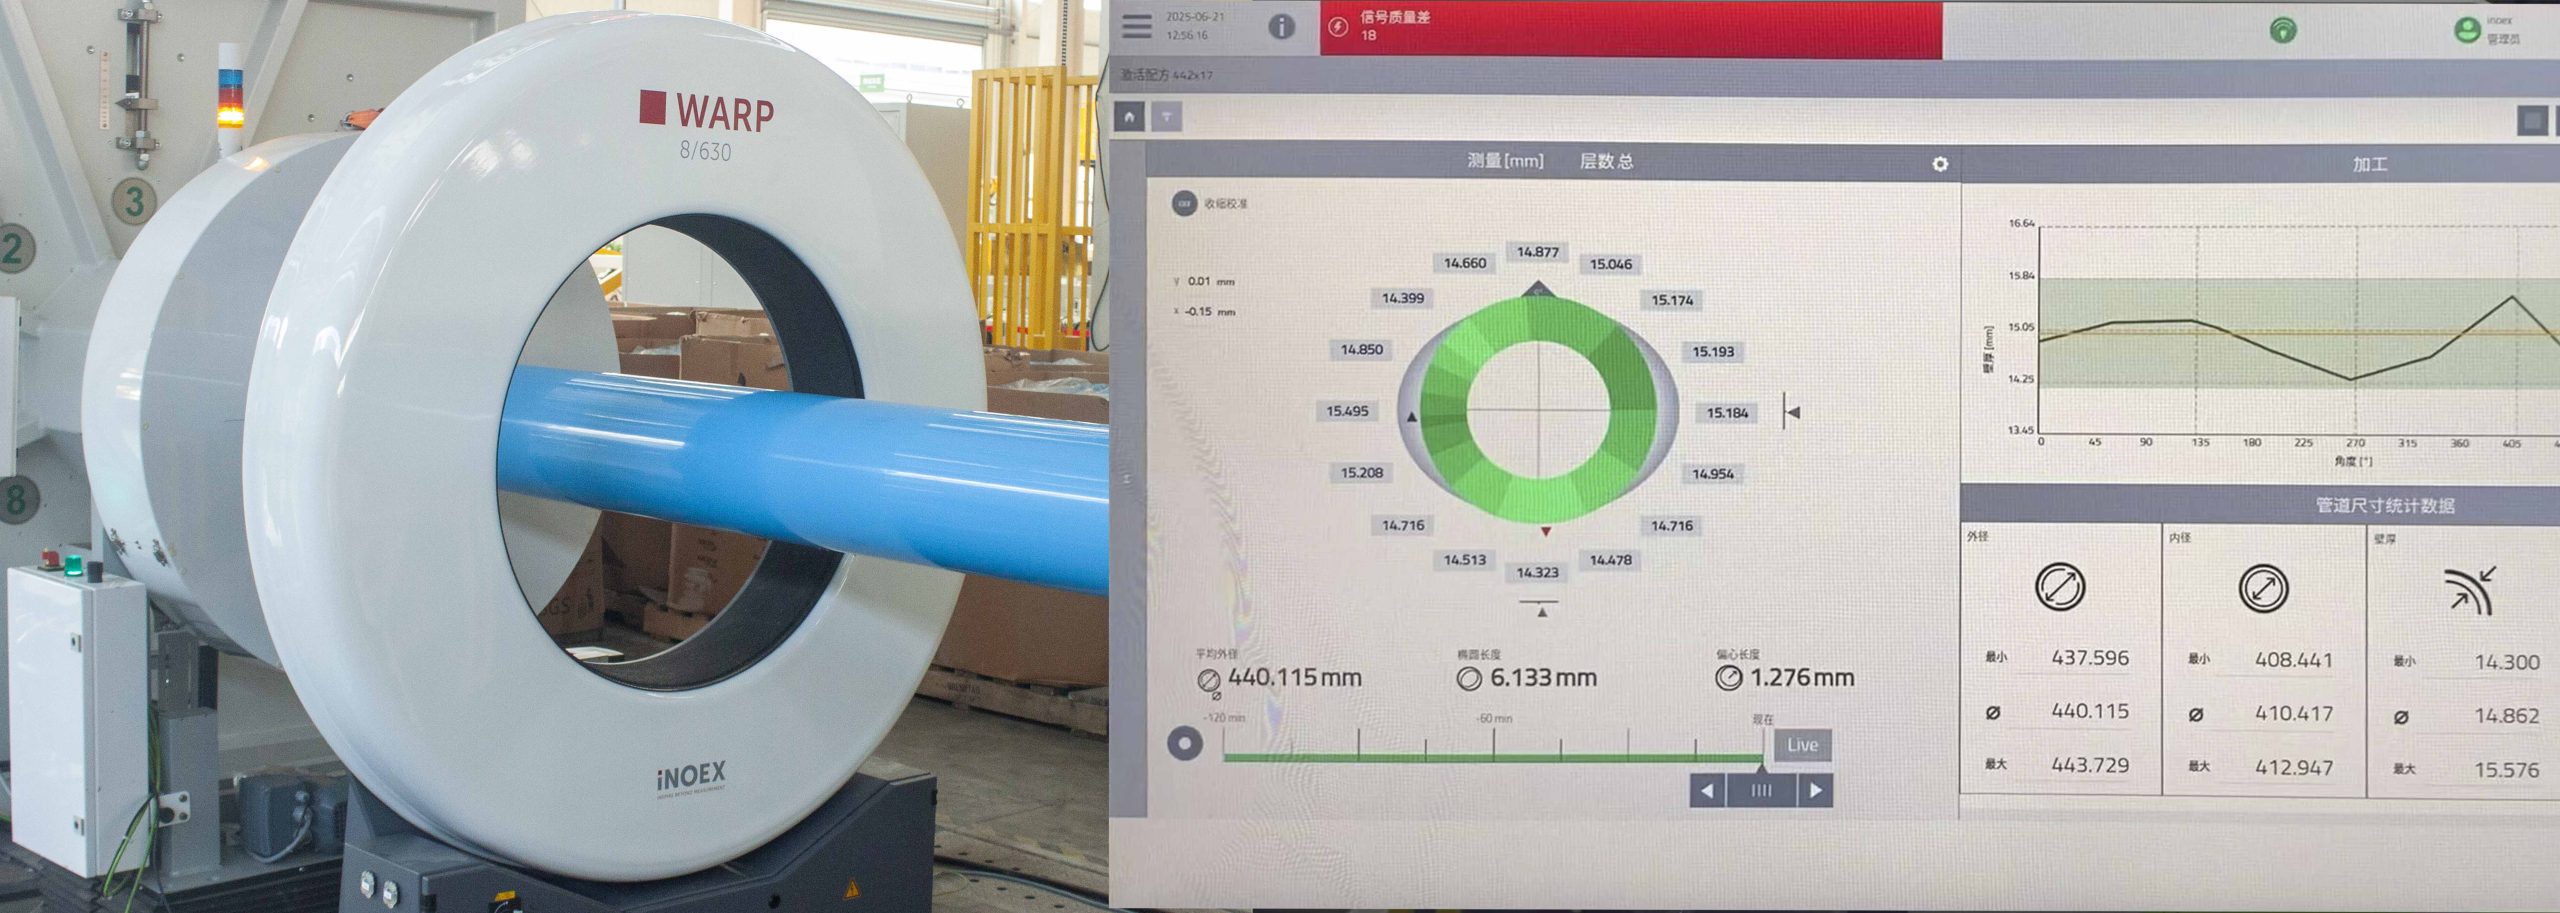
Automatic wall-thickness control
Online measurement and linked process control support consistent wall thickness through the orientation and production process.
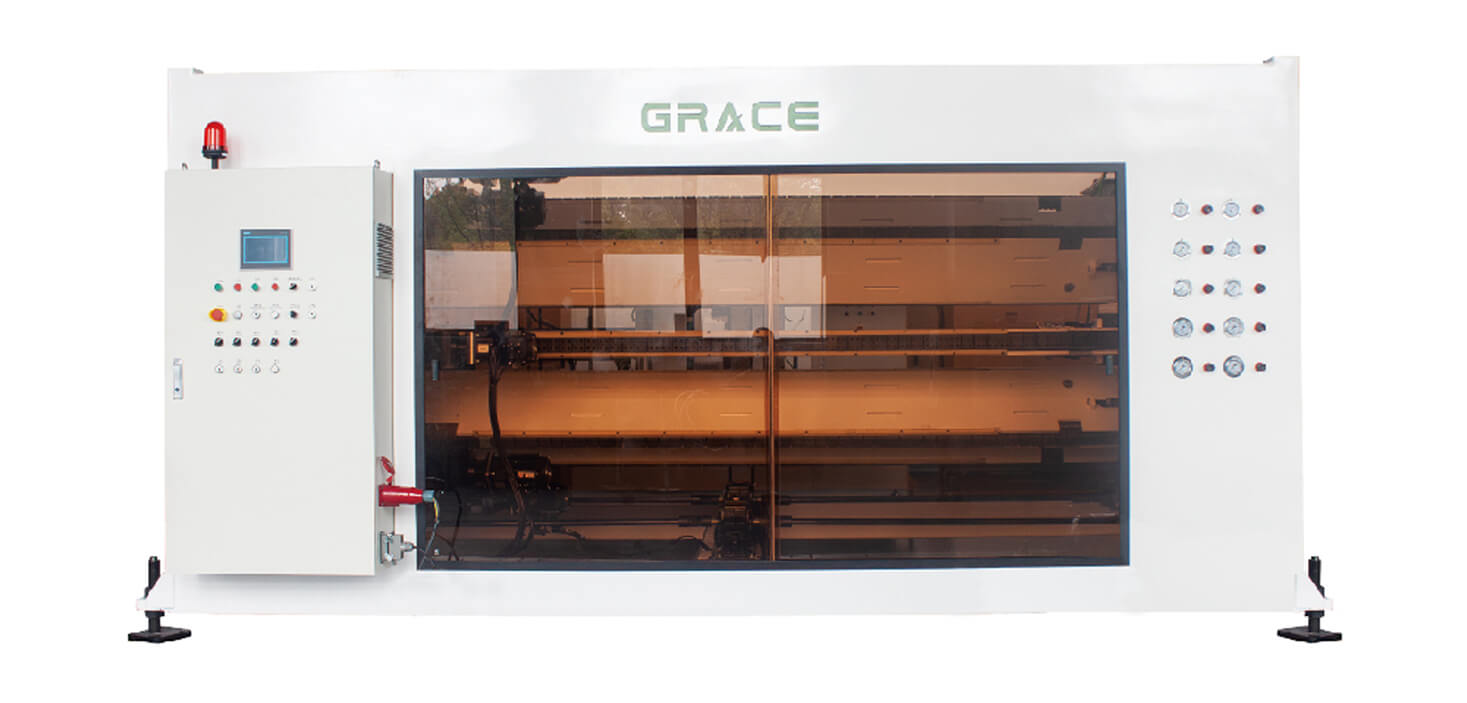 Explore this equipment →
Heavy-duty haul-off
Two coordinated haul-off units use measured tension and synchronized speed control to support stable handling through the final line stages.
View equipment page →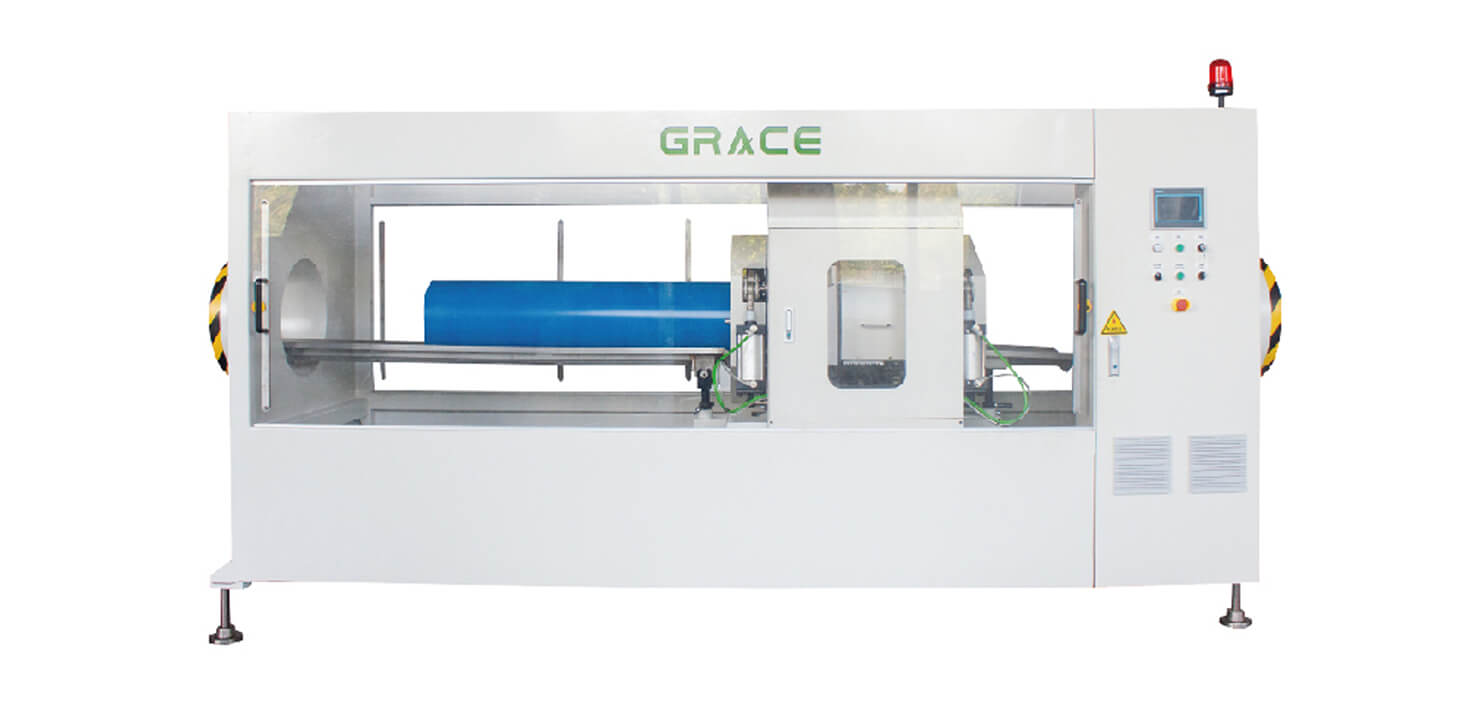 Explore this equipment →
Dust-Free Cutter
The final cutting station provides controlled positioning, secure clamping and dust collection for clean, consistent pipe ends.
View equipment page →CONFIGURATION ENGINEERING
Defining a PVC-O line through a controlled orientation project
PVC-O is not a conventional PVC line with an additional downstream module. The preform, temperature-conditioning, radial expansion, axial stretching, cooling, measurement and acceptance route are engineered as one controlled project around the target market and product schedule.
Product definition before equipment
The project begins with the applicable market requirements, complete DN × PN or wall-thickness schedule, PVC formulation and intended application. These inputs establish the product boundary before the orientation platform and tooling are defined.
Preform extrusion & conditioning
The parallel twin-screw extruder, preform die, calibration and temperature-conditioning stages are configured to establish a controlled preform before it reaches the orientation section. Tooling and temperature windows are specific to the selected product.
Integrated radial & axial orientation
Radial expansion and axial stretching are coordinated with heating, line speed and downstream handling. The process is reviewed as a connected route rather than a collection of independent machines.
Measurement & validation plan
In-line dimensional measurement, process-data recording, finished-pipe handling and the project validation route are selected together. Performance classes, certification and customer acceptance are confirmed only against the applicable project plan.
FOR A TECHNICAL PROPOSAL
Information that lets us define the right line.
- Target market, applicable standard edition and the intended PVC-O application
- Complete DN × PN or wall-thickness schedule and required product form
- PVC formulation, material class and design inputs required for the project
- Tooling, socketing, cutting, marking, handling and packing requirements
- Factory utilities, available line length, water conditions and electrical supply
- Required measurement, traceability, validation and customer-acceptance plan
Product range, output, pressure class, standards, certification and acceptance criteria are released only after project-specific technical, quality and regulatory review. Historical concepts or trial conditions are not universal performance promises.
TECHNICAL DATA
PVC-O project definition and verification matrix
| Engineering item | Project input | What must be verified |
|---|---|---|
| Applicable standard | Target market and required standard edition | Current edition, conformity route and local regulatory requirements |
| Material and formulation | PVC formulation, material class and design coefficient | Suitability for the selected orientation process and pressure class |
| Product range | Complete DN × PN or wall-thickness schedule | Platform boundary, preform geometry, finished dimensions and ovality |
| Orientation process | Preheating window, radial expansion and axial stretch requirements | Stable temperature window, expansion ratio and synchronized line control |
| Tooling package | Preform die, orientation tooling, calibrators and socketing requirements | Tooling count, shrinkage allowance, interchangeability and inspection method |
| In-line quality control | Wall-thickness, diameter and process-data requirements | Measurement range, calibration status, traceability and acceptance tolerance |
| Product validation | Pressure class and customer acceptance plan | Hydrostatic pressure, burst and applicable type tests under agreed conditions |
Applicable standard
- Project input
- Target market and required standard edition
- What must be verified
- Current edition, conformity route and local regulatory requirements
Material and formulation
- Project input
- PVC formulation, material class and design coefficient
- What must be verified
- Suitability for the selected orientation process and pressure class
Product range
- Project input
- Complete DN × PN or wall-thickness schedule
- What must be verified
- Platform boundary, preform geometry, finished dimensions and ovality
Orientation process
- Project input
- Preheating window, radial expansion and axial stretch requirements
- What must be verified
- Stable temperature window, expansion ratio and synchronized line control
Tooling package
- Project input
- Preform die, orientation tooling, calibrators and socketing requirements
- What must be verified
- Tooling count, shrinkage allowance, interchangeability and inspection method
In-line quality control
- Project input
- Wall-thickness, diameter and process-data requirements
- What must be verified
- Measurement range, calibration status, traceability and acceptance tolerance
Product validation
- Project input
- Pressure class and customer acceptance plan
- What must be verified
- Hydrostatic pressure, burst and applicable type tests under agreed conditions
PVC-O is not a conventional PVC line with a different name. Platform range, output, pressure rating, standards, certification and acceptance criteria are released only after project-specific technical, quality and regulatory review. Historical concepts or trial parameters are not contractual performance guarantees.