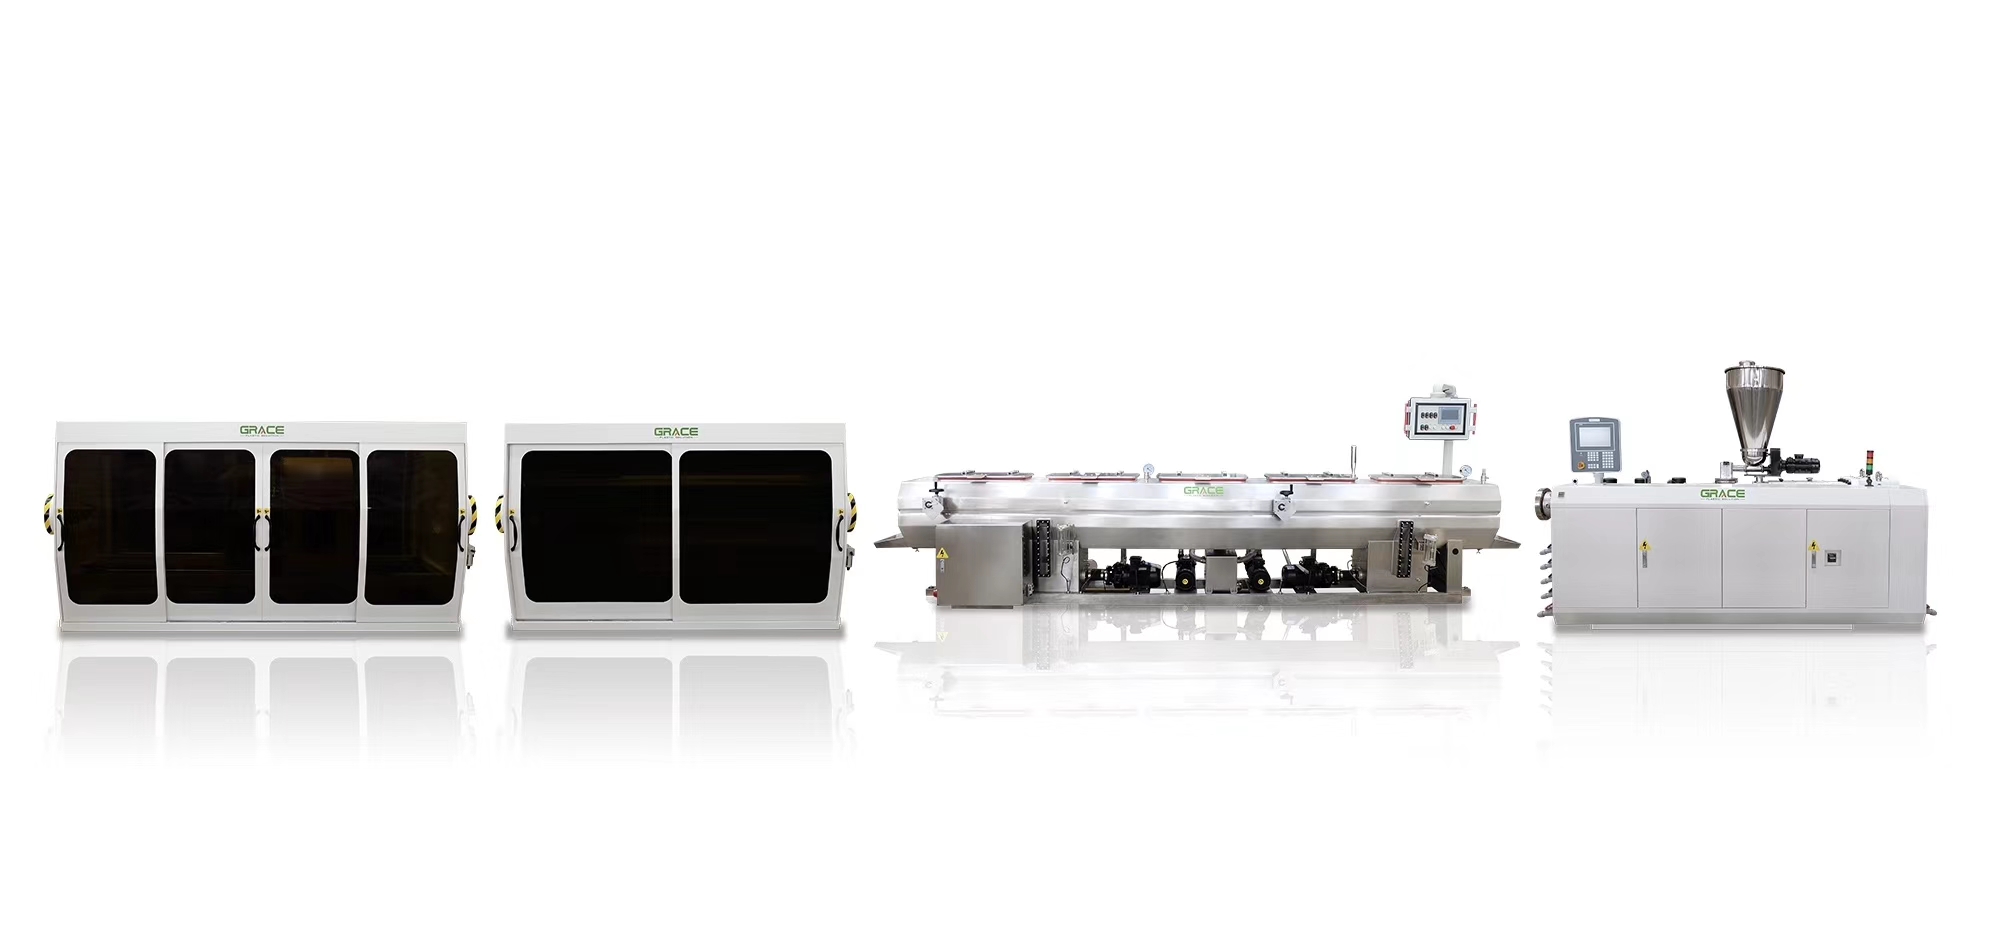
SEE IT IN OPERATION
PVC Pipe Extrusion Line
Start with the equipment in operation, then explore the principal functions and the relevant technical configuration.
PRODUCT OVERVIEW
Designed around the production task.
Complete PVC pipe extrusion systems for reliable output, dimensional control and practical day-to-day operation.
EQUIPMENT REFERENCE
Confirmed equipment, followed by the process context.
 Explore this equipment →
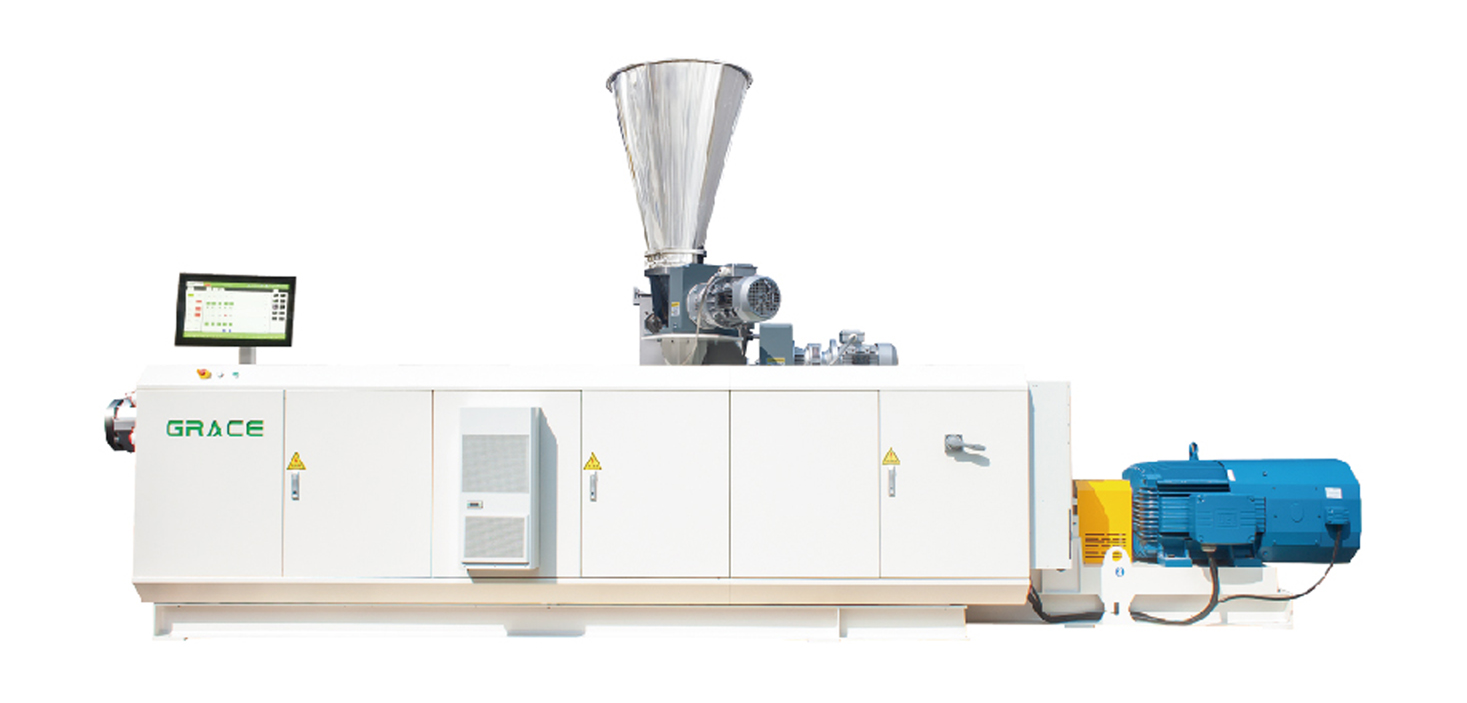
Parallel twin-screw extruder
The 36 L/D parallel twin-screw extruder is configured for stable PVC plasticization, controlled melt temperature and practical output across a wide range of pipe specifications.
View equipment page →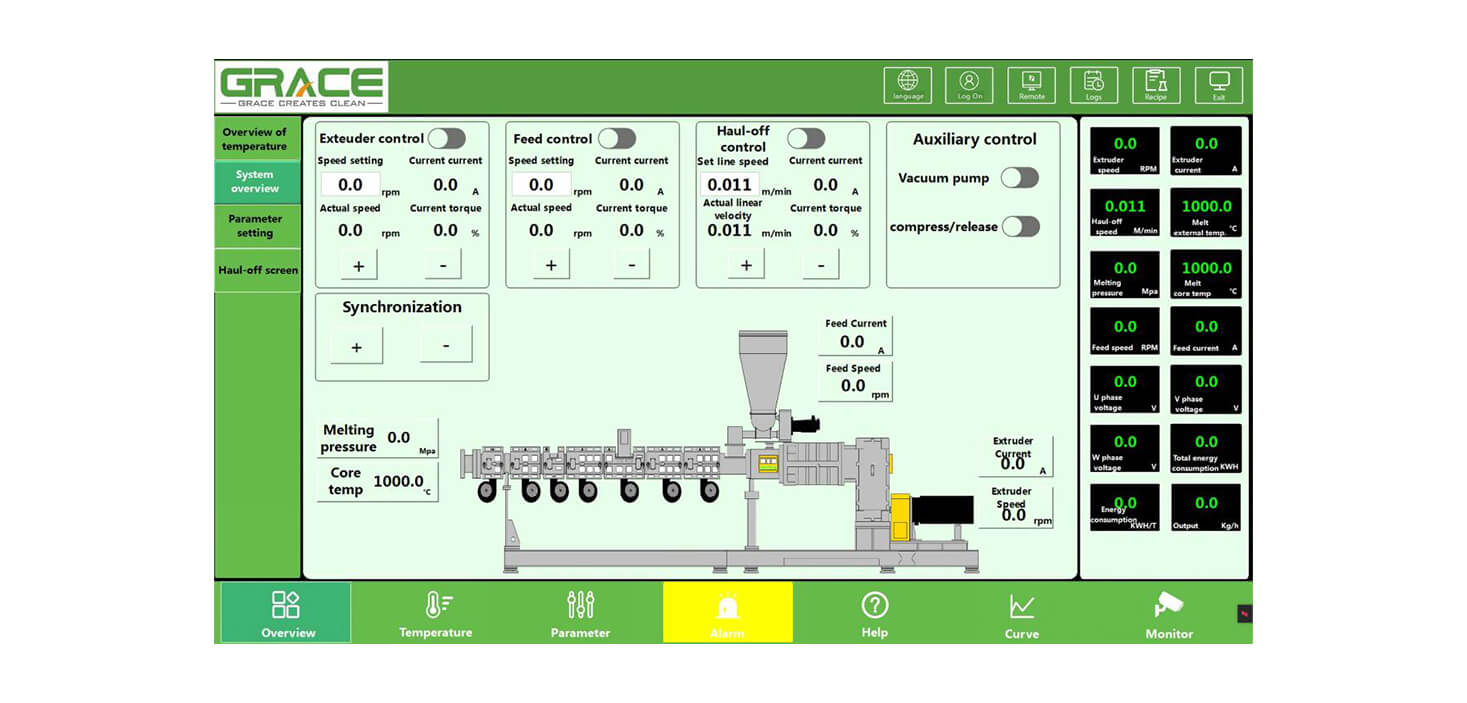
PLC control system
A unified operator interface brings together speed, temperature and pressure data, supporting recipe management, day-to-day monitoring and coordinated line operation.
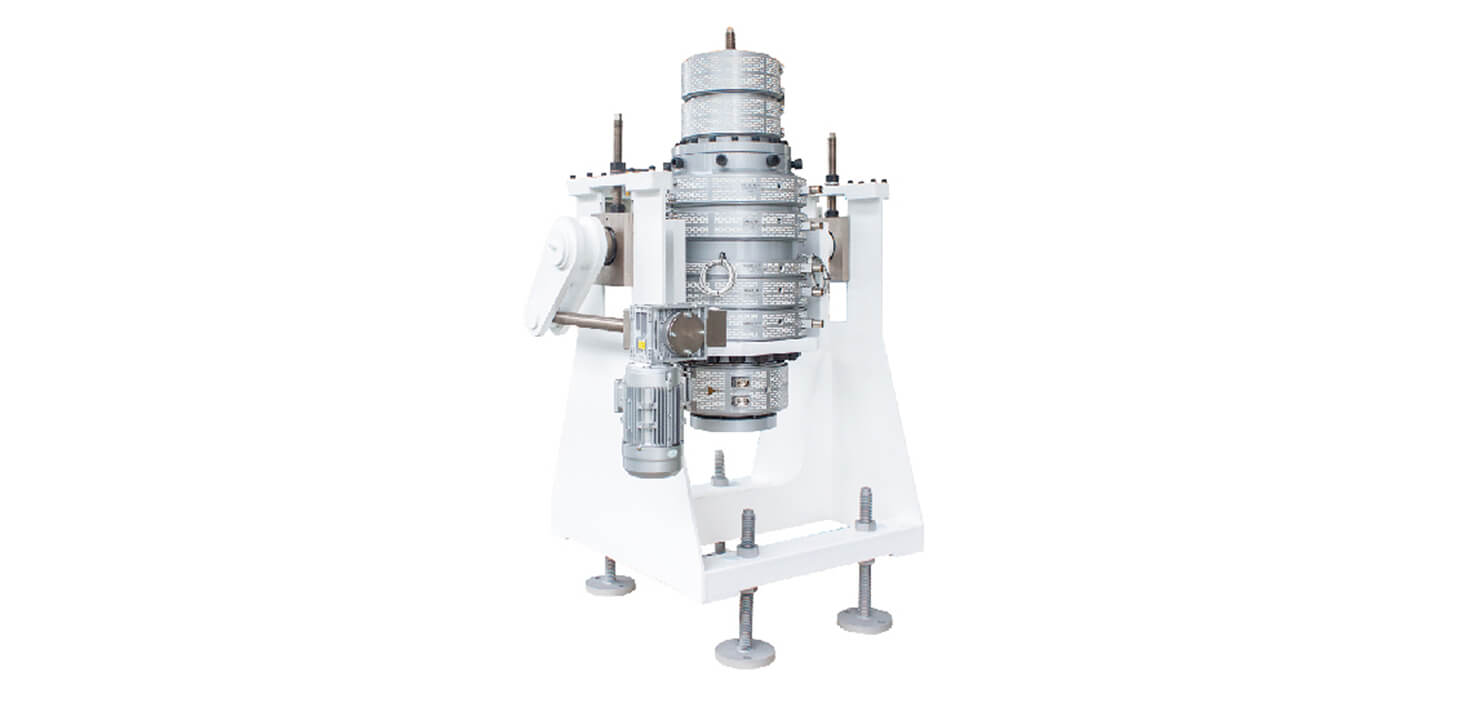
Die head
The die-head flow path and temperature-control arrangement are designed to support even wall-thickness distribution, a stable melt profile and dependable pipe quality.
 Explore this equipment →
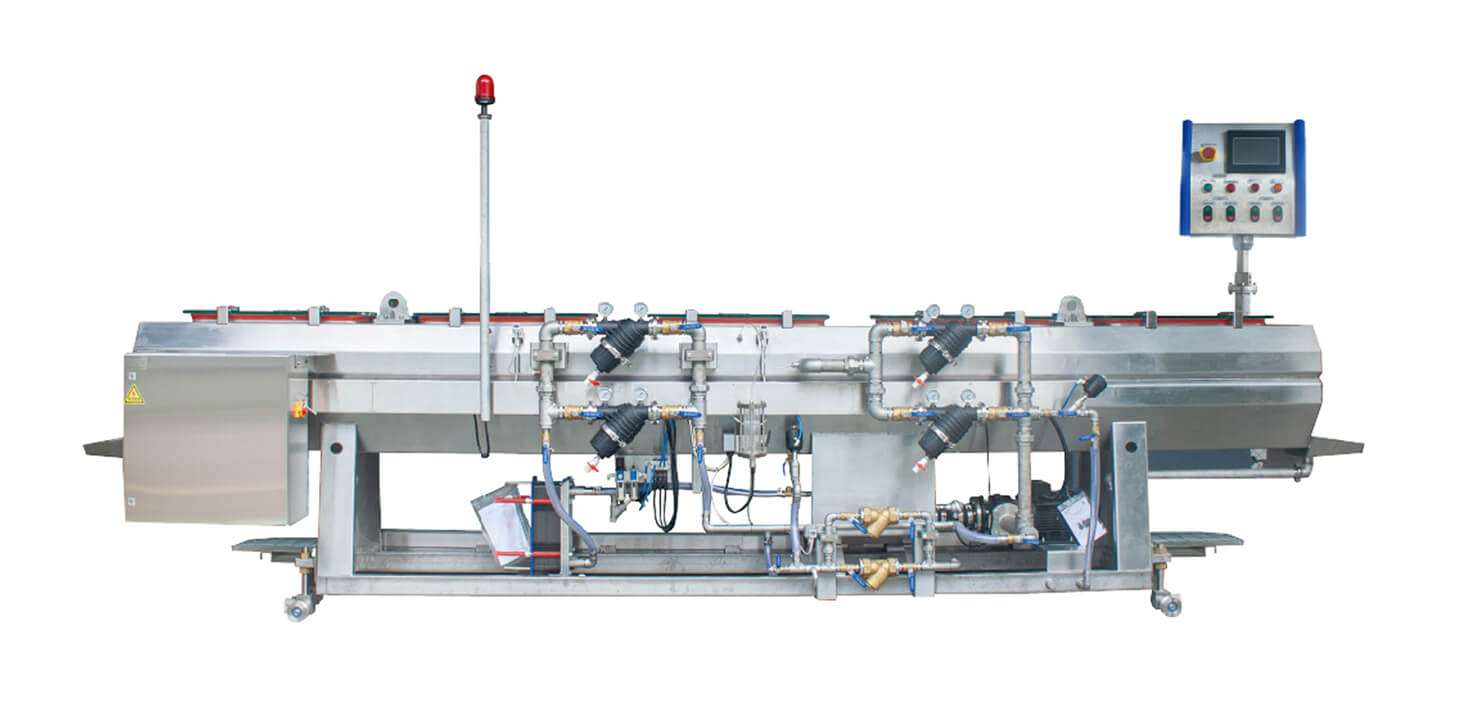
Vacuum tank
Variable-frequency vacuum control, efficient filtration and adjustable spray cooling are configured to support stable calibration, reliable water management and practical energy use.
View equipment page →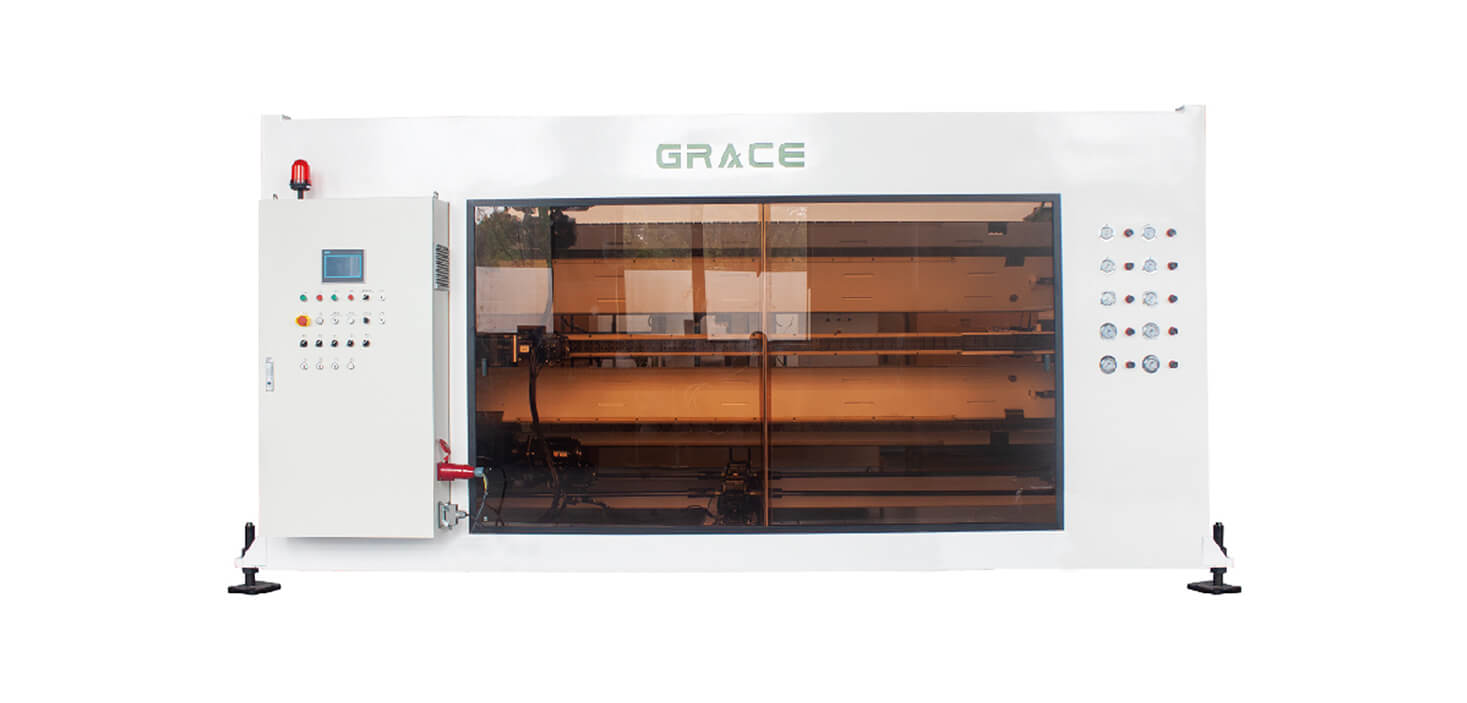 Explore this equipment →
Haul-off
The haul-off unit provides controlled traction and synchronized caterpillar movement to protect pipe geometry as the product moves through the downstream process.
View equipment page →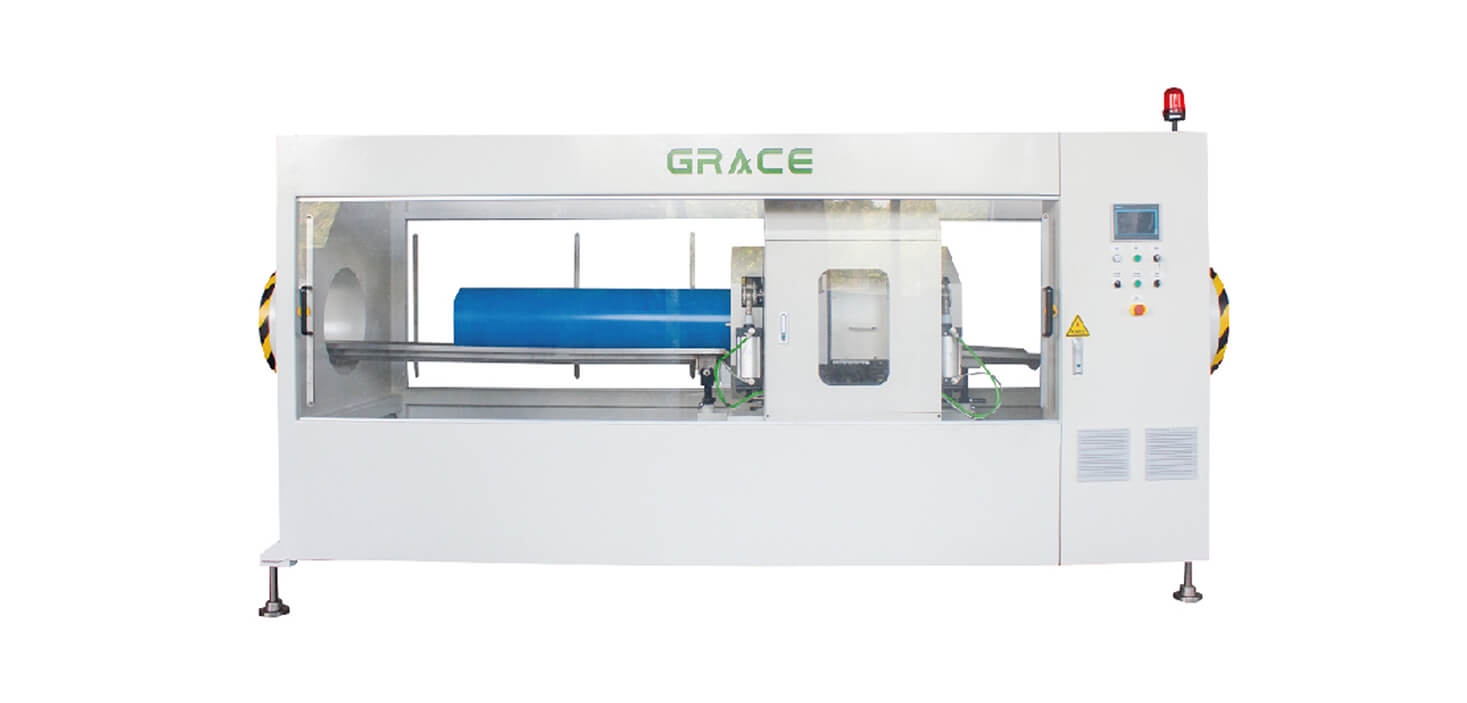 Explore this equipment →
Dust-Free Cutter
The dust-free cutter combines secure clamping with controlled cutting and chip collection to support clean pipe ends, efficient recycling of chips and safe operation.
View equipment page →CONFIGURATION ENGINEERING
Engineering a PVC pipe line from the complete pipe schedule
A reliable PVC pipe line is selected from the full production task — not from pipe diameter alone. The material formulation, complete OD × wall-thickness schedule, number of outlets, target operating rate, factory layout and downstream finishing requirement are reviewed together before the equipment is defined.
Material & product definition
PVC resin grade, stabiliser system, filler level, intended application, applicable standard and the complete pipe schedule establish the starting point. The relevant schedule should include every outside diameter with its wall thickness or SDR / PN requirement, not only the largest pipe.
Extrusion & tooling package
The 36 L/D parallel twin-screw platform, die head and calibration tooling are matched to the selected PVC formulation and pipe schedule. A line may use one, two or multiple outlets when the product range and production objective support that arrangement.
Cooling & downstream balance
Vacuum sizing, spray cooling, haul-off and cutting are engineered as one connected section. Tank quantity and effective cooling length, water conditions, available factory length, traction arrangement and cutting cycle must support the selected pipe and operating rate together.
Automation & finishing options
Line controls, dosing and handling functions, measurement requirements, marking, pipe-end finishing and collection equipment are selected around the project. Each option is reviewed for its effect on product handling, changeover work and the final line layout.
FOR A TECHNICAL PROPOSAL
Information that lets us define the right line.
- PVC formulation and material information, including the stabiliser and filler system where applicable
- Complete OD × wall-thickness / SDR / PN schedule and intended pipe application
- Target production rate for each key specification and required number of outlets
- Pipe length, cutting, chamfering, socketing, marking, handling and packing requirements
- Factory effective length, water temperature and flow, electrical supply, compressed air and site conditions
- Required automation, measurement, control-brand, certification and service expectations
The configuration table below is a representative planning guide, not a universal promise. Final output, energy use, cooling length, tooling, quality criteria and contractual performance are confirmed only through project-specific technical review and FAT criteria.
TECHNICAL DATA
Representative PVC pipe line configurations
| Platform | Pipe range | Outlets | Extruder configuration | Typical output |
|---|---|---|---|---|
| PVC 63 Dual-strand | DN20–63 | 2 | GMPT75/36-A45 | 350–500 kg/h |
| PVC 110 Dual-strand | DN20/32–110 | 2 | GMPT90/36-A75 | 640–800 kg/h |
| PVC 160 | DN50–160 | 1 | GMPT75/36-A45 | 400–500 kg/h |
| PVC 250 | DN110–250 | 1 | GMPT75/36 or 90/36 | 400–800 kg/h |
| PVC 315 | DN160–315 | 1 | GMPT90/36 or 114/36 | 640–1,200 kg/h |
| PVC 450 | DN250–450 | 1 | GMPT90/36 or 114/36 | 640–1,200 kg/h |
| PVC 630 | DN315–630 | 1 | GMPT114/36-A110 | 960–1,200 kg/h |
| PVC 800 | DN400–800 | 1 | GMPT114/36 or 135/36 | 960–1,600 kg/h |
| PVC 1200 | DN630–1,200 | 1 | GMPT114/36 or 135/36 | 960–1,600 kg/h |
PVC 63 Dual-strand
- Pipe range
- DN20–63
- Outlets
- 2
- Extruder configuration
- GMPT75/36-A45
- Typical output
- 350–500 kg/h
PVC 110 Dual-strand
- Pipe range
- DN20/32–110
- Outlets
- 2
- Extruder configuration
- GMPT90/36-A75
- Typical output
- 640–800 kg/h
PVC 160
- Pipe range
- DN50–160
- Outlets
- 1
- Extruder configuration
- GMPT75/36-A45
- Typical output
- 400–500 kg/h
PVC 250
- Pipe range
- DN110–250
- Outlets
- 1
- Extruder configuration
- GMPT75/36 or 90/36
- Typical output
- 400–800 kg/h
PVC 315
- Pipe range
- DN160–315
- Outlets
- 1
- Extruder configuration
- GMPT90/36 or 114/36
- Typical output
- 640–1,200 kg/h
PVC 450
- Pipe range
- DN250–450
- Outlets
- 1
- Extruder configuration
- GMPT90/36 or 114/36
- Typical output
- 640–1,200 kg/h
PVC 630
- Pipe range
- DN315–630
- Outlets
- 1
- Extruder configuration
- GMPT114/36-A110
- Typical output
- 960–1,200 kg/h
PVC 800
- Pipe range
- DN400–800
- Outlets
- 1
- Extruder configuration
- GMPT114/36 or 135/36
- Typical output
- 960–1,600 kg/h
PVC 1200
- Pipe range
- DN630–1,200
- Outlets
- 1
- Extruder configuration
- GMPT114/36 or 135/36
- Typical output
- 960–1,600 kg/h
Typical outputs are configuration-dependent, not unconditional contractual guarantees. Final output must be verified against PVC formulation, pipe dimensions and wall thickness, number of outlets, cooling conditions, haul-off capability and cutting cycle. Contractual guarantees are subject to project-specific technical approval and FAT criteria. The PVC 1200 platform, including the GMMJ1900 die, remains a custom-engineered rather than fully standard configuration.